.svg)
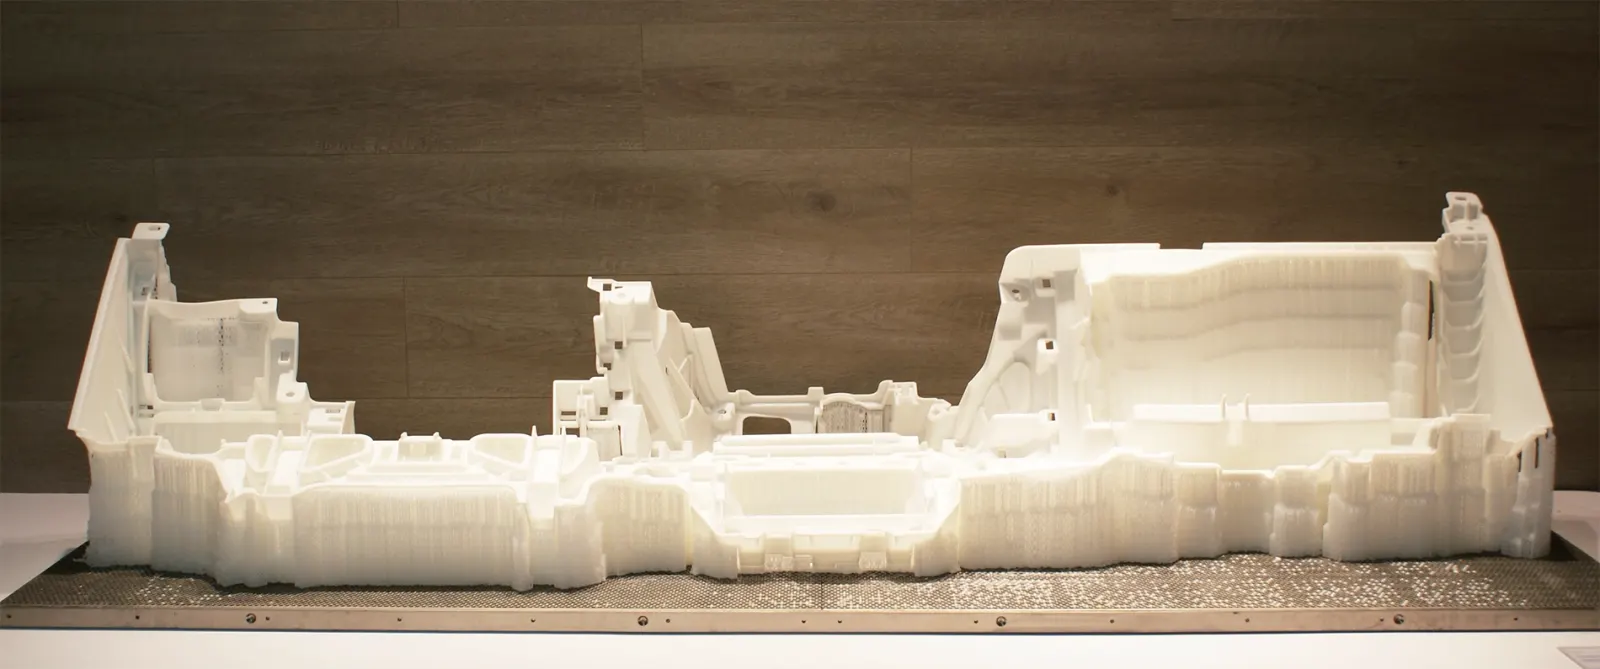
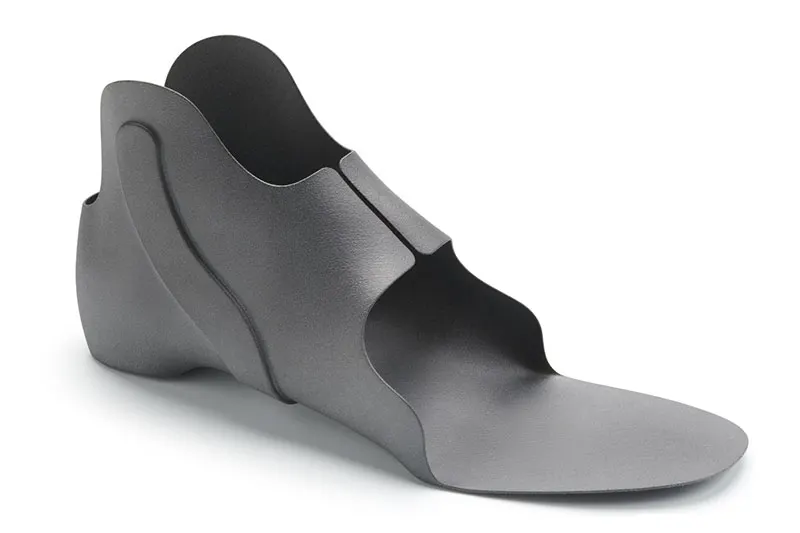
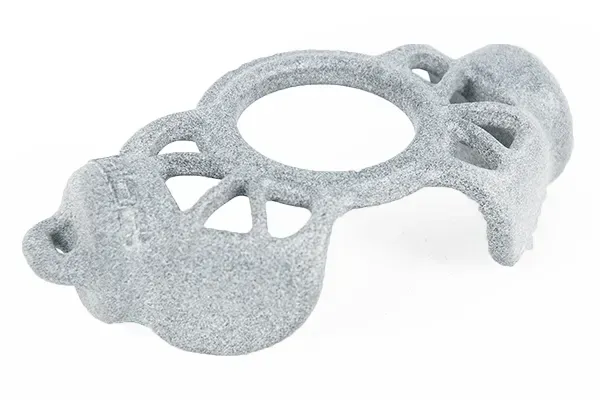
4–6 days lead time
Raw grey
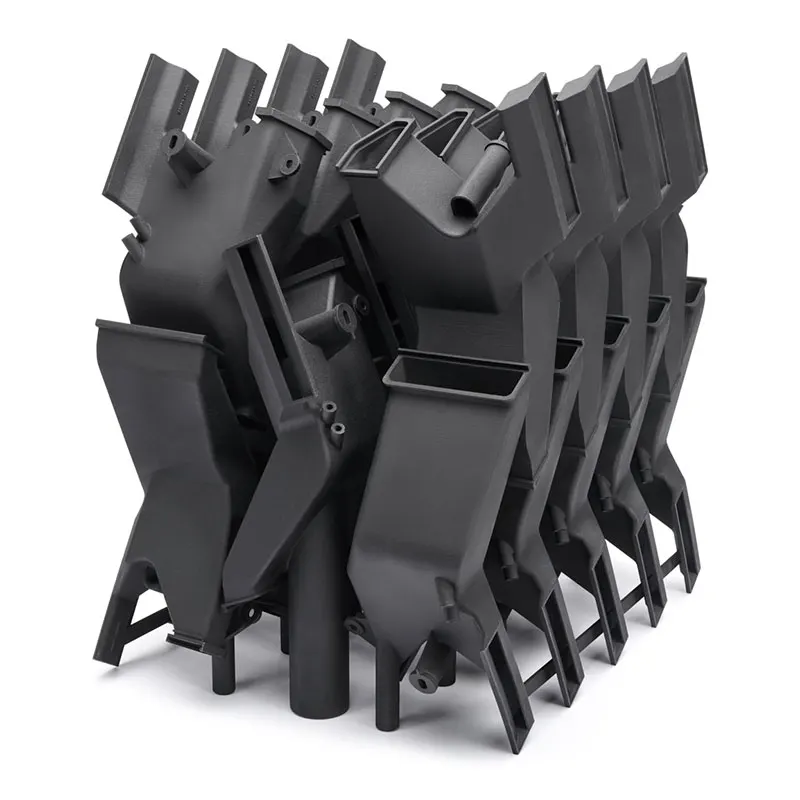
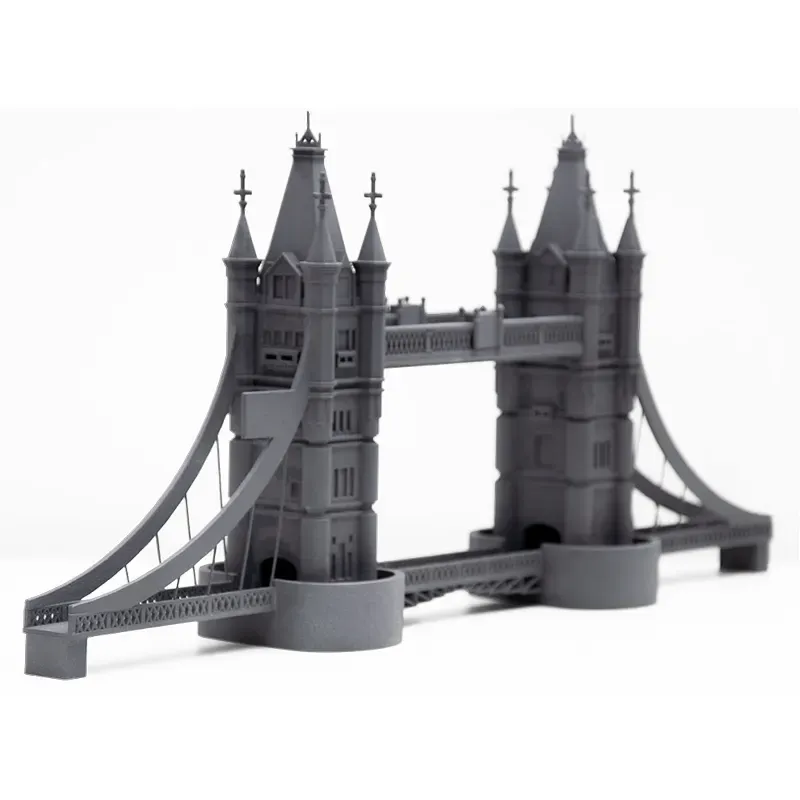
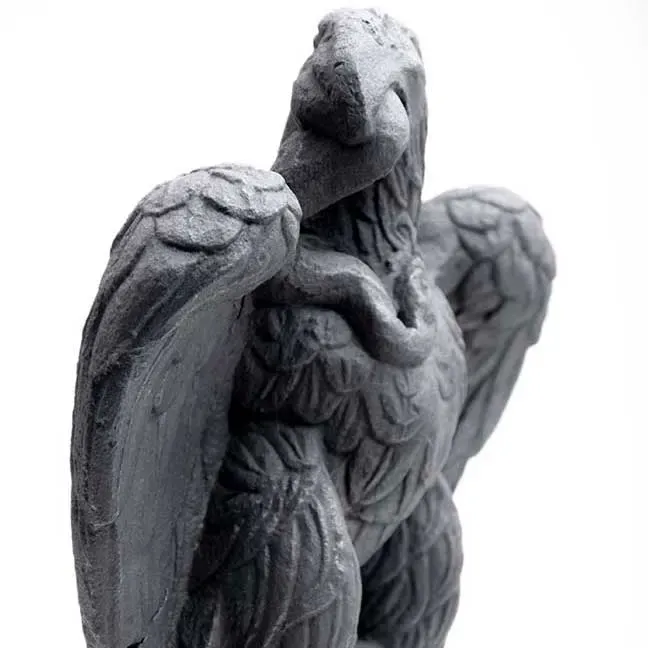
No further treatment. Loose powder is removed with DyeMansion equipment, leaving crisp parts with a grain-like texture and mottled grey colour.
Engineering resins for the Reflex 3D printers
The workhorse resins for UnionTech 3D printers
Castables, elastomers, tooling and clear resins
Production nylon — strong, isotropic, no supports
Fine detail and smooth surfaces
Orthotics, vehicle parts, one-off replicas
Printed products and replacements, in the shop today
Components nobody makes any more, made again
Tell us about a part you cannot buy
Parts printed in our own bureau
3D printing service · HP Multi Jet Fusion
Production runs, prototypes and bespoke parts in PA12 or PA11 nylon, from our own machines in Cheshire. Thousands of parts in a single twelve hour build, with no tooling to pay for first.
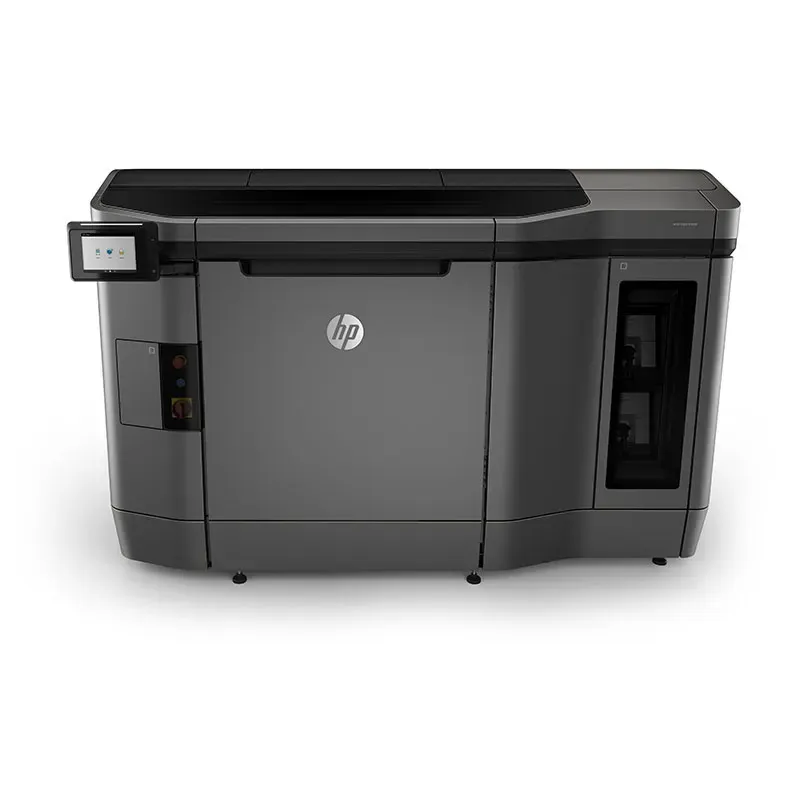
An inkjet printhead deposits droplets of fusing and detailing agents onto a fine layer of nylon powder. Heat lamps then activate the agents, fusing the powder into a solid layer. The next layer goes down on top.
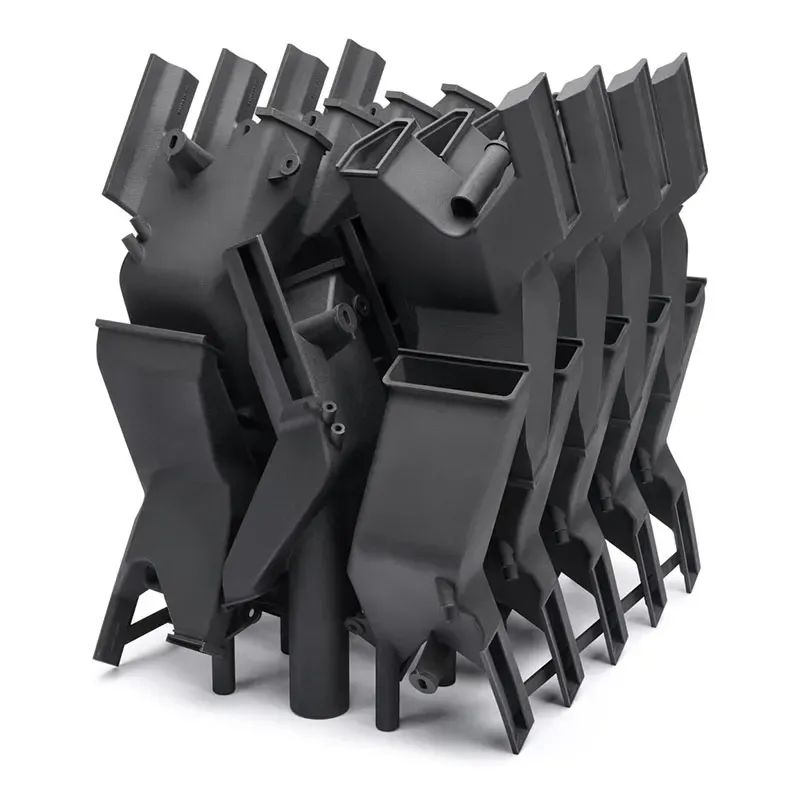
The powder supports the part as it builds, so complex geometries and internal channels need no support structures. Parts come out accurate, detailed and isotropic. They have the same strength in X, Y and Z.
Parts can be left their natural grey or dyed black. They can also be smoothed with vibro finishing.
At a glance
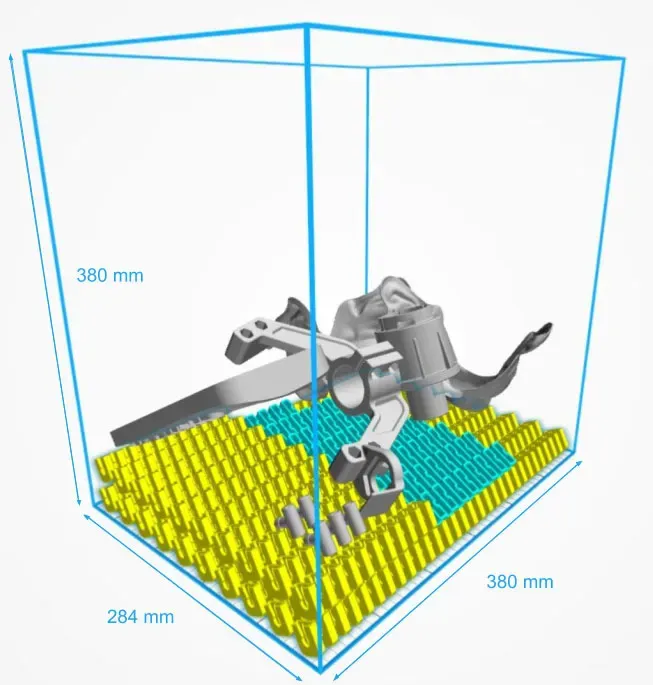
Thousands of end-use parts in one build, with no tooling cost and a lower cost per part.
Product variations, or parts that are each different, produced at volume.
Accurate, detailed prototypes with a fast turnaround to cut development time.
Insoles, AFOs, wrist braces and helmets in batches, in PA12 or PA11.
Ordered by lead time, because that is usually what decides it. All four start from the same printed part.
4–6 days lead time
No further treatment. Loose powder is removed with DyeMansion equipment, leaving crisp parts with a grain-like texture and mottled grey colour.
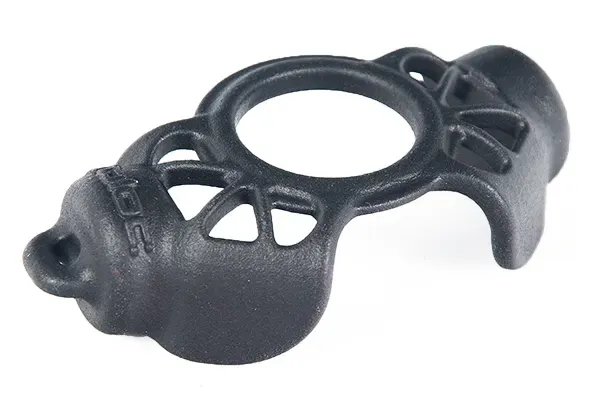
5–7 days lead time
Dyed deep black for a tough, durable, scratch-resistant finish.
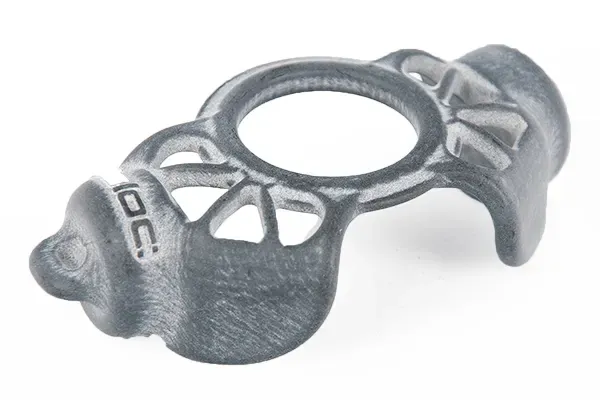
6–8 days lead time
Smoothed in a vibro tumbling process. The parts keep their raw grey colour.
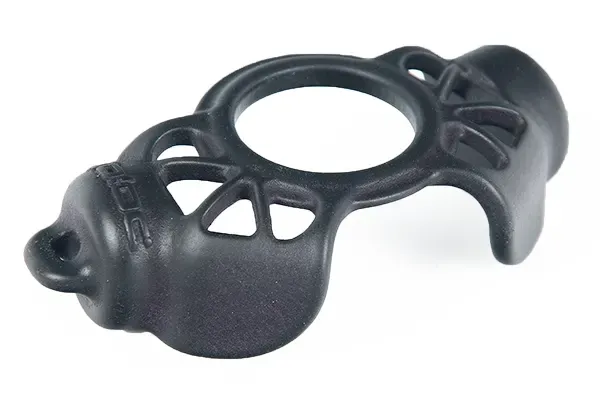
7–9 days lead time
A smooth vibro-polished surface in a deep, scratch-resistant black.
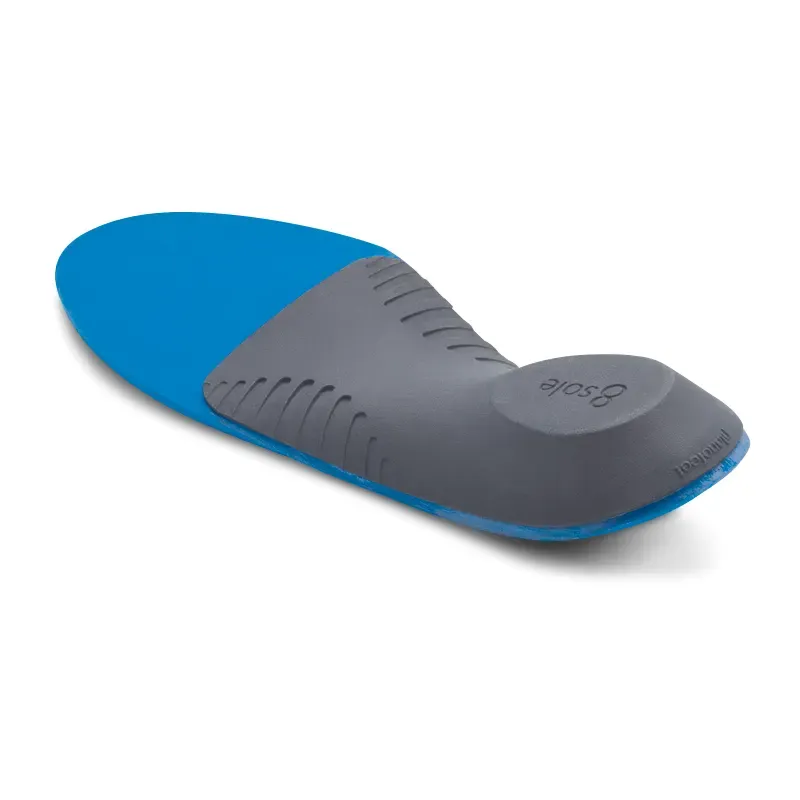
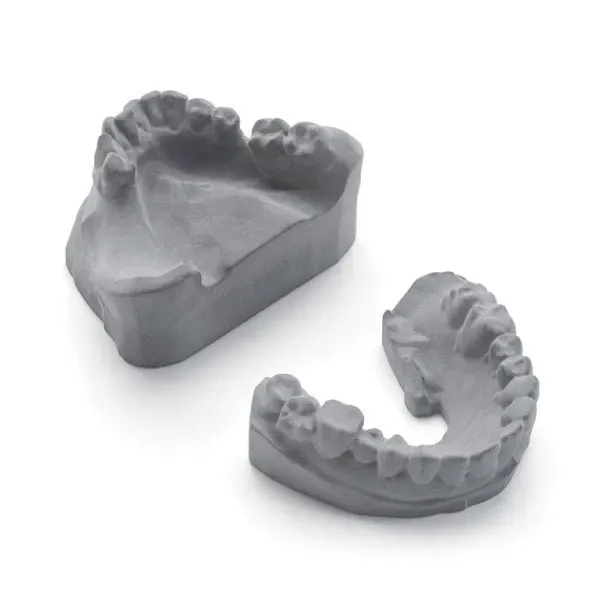
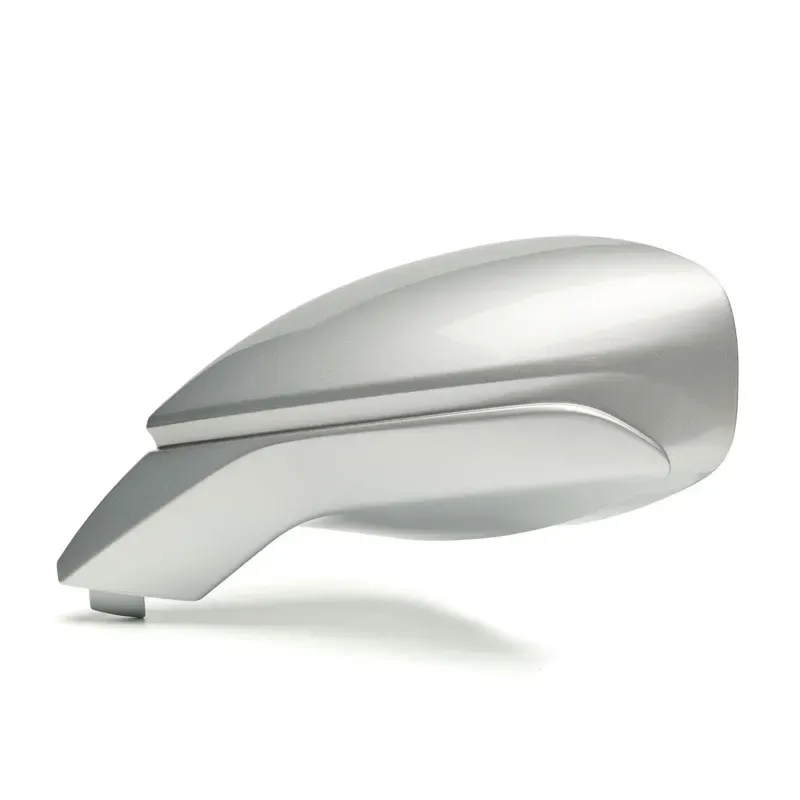
Both run on our own HP 3D printers. Not sure which? Tell us what the part does.
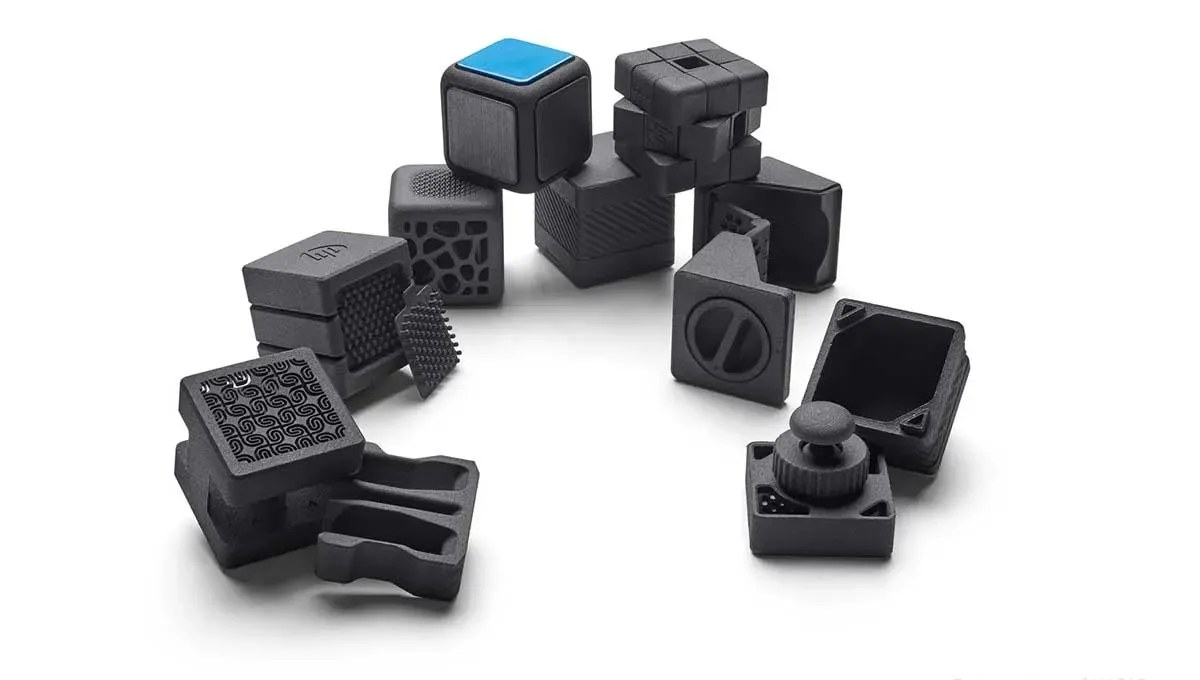
Strong, durable and accurate. Isotropic properties in X, Y and Z. The right choice when many thousands of parts are needed.
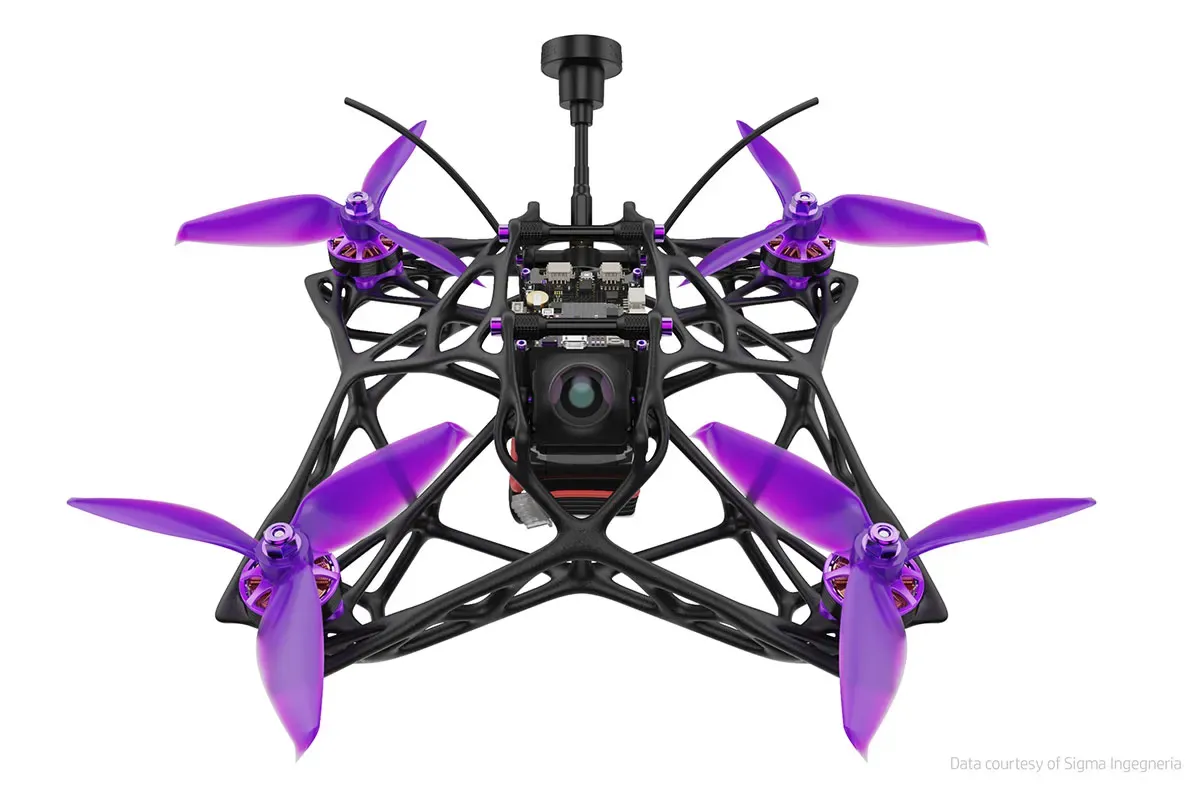
Strong yet flexible, with high impact resistance and elongation at break. Snap fits, insoles, sports goods and living hinges.
An end-to-end job using 3D scanning and printing to make a storage box for a triathlon racing bike.
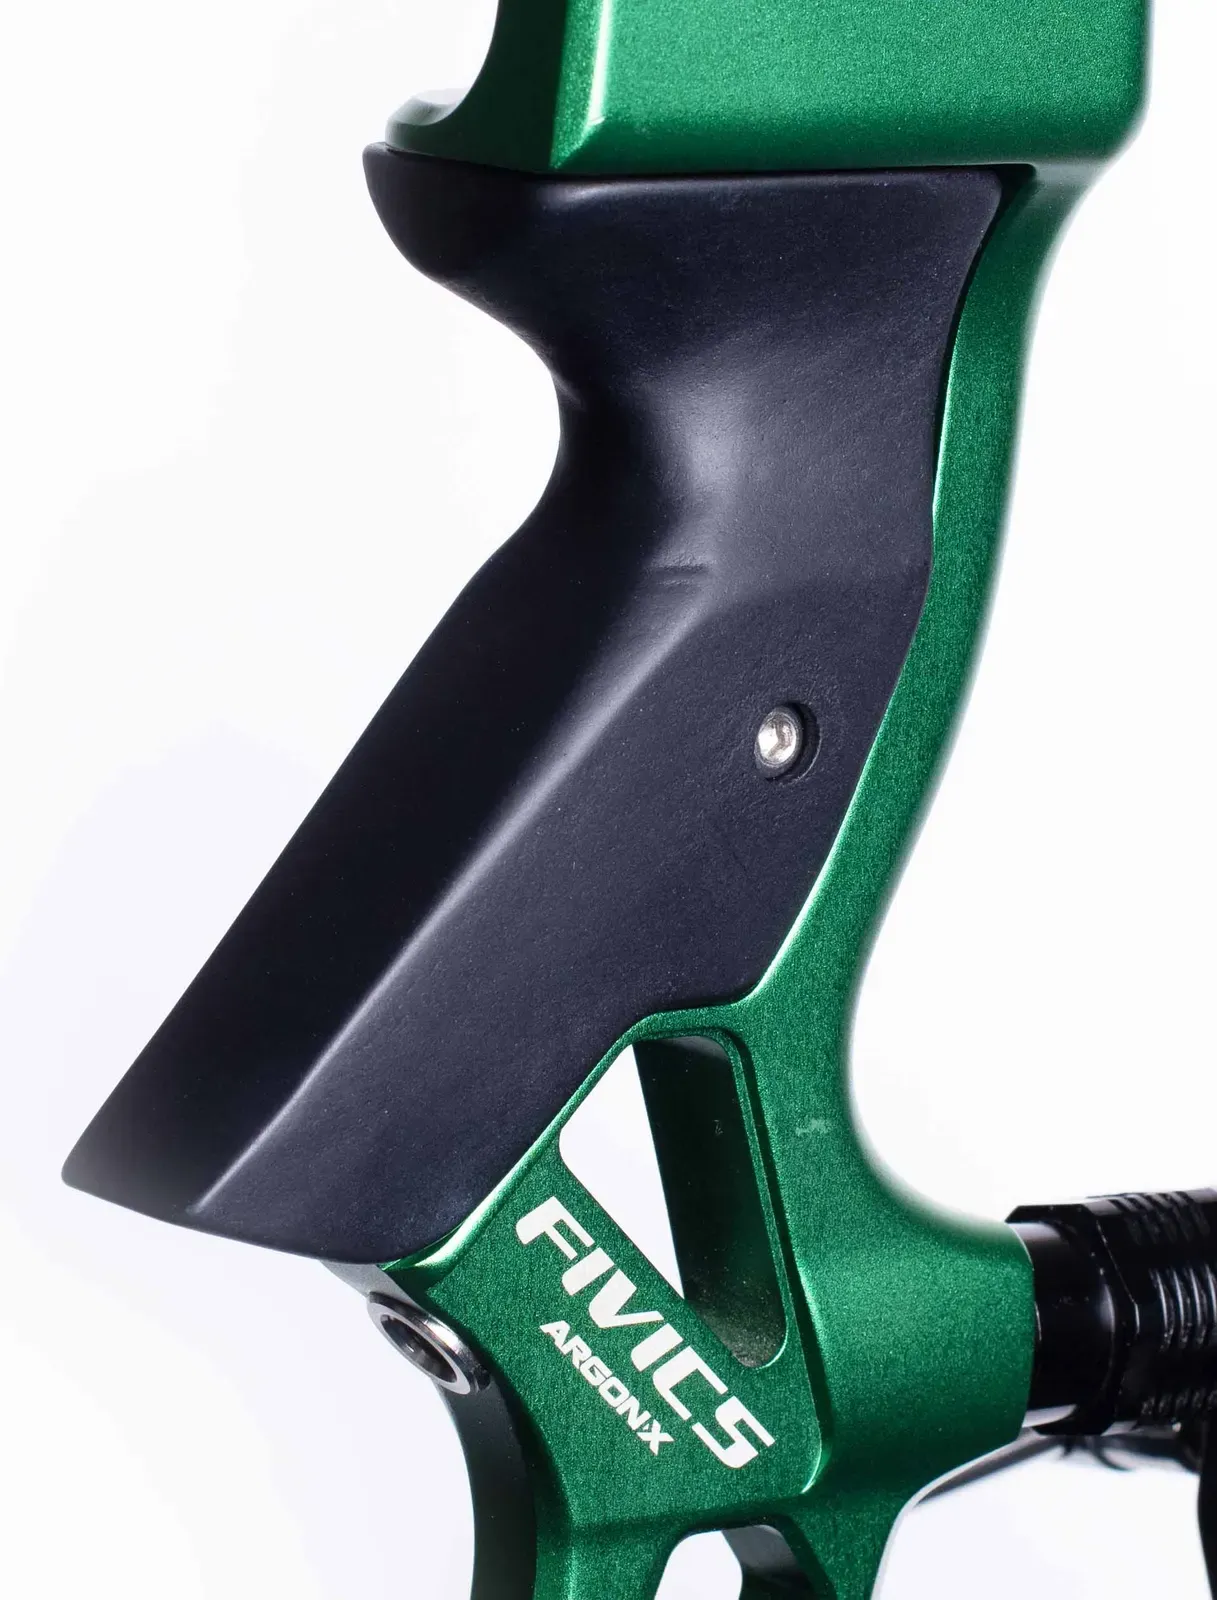
Digitising a custom archery grip and printing it in PA12 nylon.
Not answered here?
Ask the engineers who run the machines. We answer the same working day.
PA12 is the choice for strong, quality parts at the lowest cost per part. PA11 offers superb impact resistance as well as elongation at break, so it suits snap fits, insoles, sports goods and living hinges.
Four: raw grey, dyed black, vibro smoothed, or dyed black and vibro smoothed. Raw parts are cleaned of loose powder using DyeMansion technology. They have a grain-like texture and mottled grey colour.
It depends on the finish: 4 to 6 days for raw grey, 5 to 7 days for dyed black, 6 to 8 days for vibro smoothing. Dyed black and vibro smoothed takes 7 to 9 days.
The build volume is 380 x 380 x 284 mm, the minimum feature size is 0.5 mm and the build layer is 80 microns.
Many thousands of parts can be made in a single 12 hour build, which is why MJF suits volume production runs of end-use parts.
No. The HP Jet Fusion process is self-supporting, so highly detailed parts with complex internal geometries can be built without support structures.
Yes. MJF nylon parts have isotropic properties in the X, Y and Z directions. They also have excellent temperature and chemical resistance. PA12 nylon
Both. For example, after prototyping we put a first batch of 100 triathlon bike storage boxes into production in PA12 nylon on HP MJF. Triathlon bike storage case study
Upload the file to our instant quote, choose the material and the quantity and the price comes back on screen. Order it there and then.
Opens our quoting tool in a new tab. Want advice on the material or process first? Contact us or ring 0330 229 0175.